Contact Us
24/7 Online Customer Support
Product Introduction
Product Description
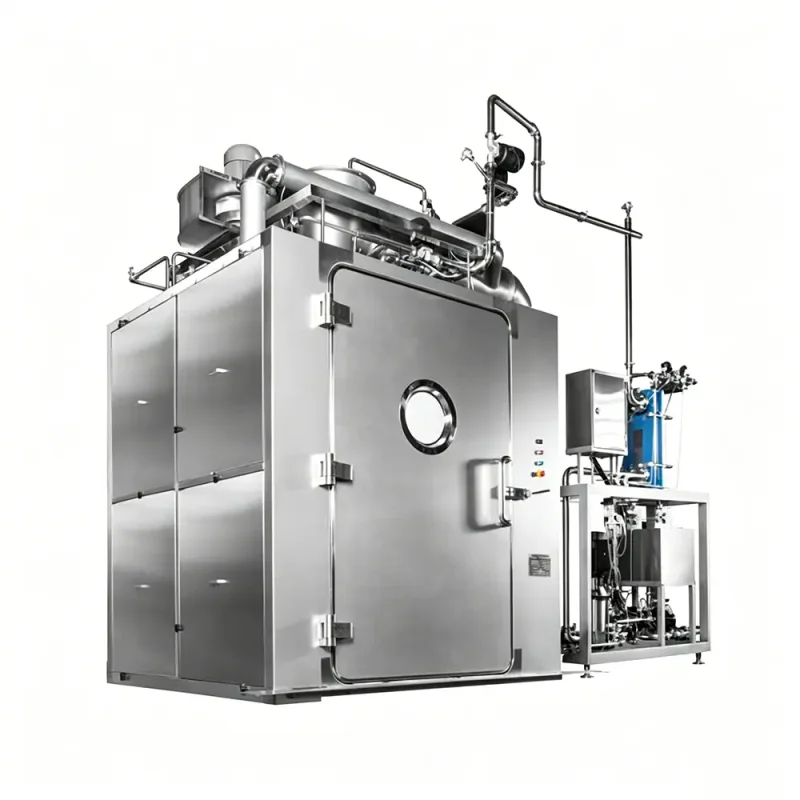
Our automated IBC container cleaning system is specifically designed for the fully automated cleaning of intermediate bulk containers (IBCs), blending bins, and transfer bins used in solid dosage form production in the pharmaceutical industry. The system provides a comprehensive and efficient cleaning solution to ensure compliance with stringent hygiene standards. It is also suitable for applications in the chemical and food industries.
Application
-
Specifically designed for the automated cleaning of IBC containers, blending bins, and transfer bins.
-
Ensures consistent and reliable cleaning performance to meet critical hygiene requirements.
Working Principle
The system consists of a cleaning chamber, pumping station, air handling unit, and PLC-based control system. The operating procedure is as follows:
-
Open the inlet door and load the IBC container or bin to be cleaned into the cleaning chamber.
-
Close the cleaning chamber door.
-
Set the cleaning program via the PLC control panel according to process requirements.
-
Start the automatic cleaning cycle.
-
After cleaning is complete, open the outlet door and remove the cleaned IBC container or bin.
-
Transfer the cleaned container to the intermediate holding station for storage.
Key Features and Benefits
-
Fully Automated: The PLC control system ensures consistent, unattended cleaning operations.
-
High Efficiency: The automated process minimizes downtime and increases throughput.
-
GMP Compliant: Designed with smooth surfaces, no dead corners, and no exposed screws to meet GMP standards for pharmaceutical manufacturing.
-
Versatility: Compatible with IBC containers, blending bins, and transfer bins of various specifications and types.
-
Advanced Air Handling: An integrated air handling unit ensures proper drying and contamination control.
-
Robust Construction: Durable design and stable performance ensure reliable operation.
-
User-Friendly Interface: An intuitive PLC control panel simplifies operation and programming.
-
Optimized Production Process: Automated cleaning process, streamlining production.
Technical Parameters
Product Description
Our automated IBC container cleaning system is specifically designed for the fully automated cleaning of intermediate bulk containers (IBCs), blending bins, and transfer bins used in solid dosage form production in the pharmaceutical industry. The system provides a comprehensive and efficient cleaning solution to ensure compliance with stringent hygiene standards. It is also suitable for applications in the chemical and food industries.
Application
-
Specifically designed for the automated cleaning of IBC containers, blending bins, and transfer bins.
-
Ensures consistent and reliable cleaning performance to meet critical hygiene requirements.
Working Principle
The system consists of a cleaning chamber, pumping station, air handling unit, and PLC-based control system. The operating procedure is as follows:
-
Open the inlet door and load the IBC container or bin to be cleaned into the cleaning chamber.
-
Close the cleaning chamber door.
-
Set the cleaning program via the PLC control panel according to process requirements.
-
Start the automatic cleaning cycle.
-
After cleaning is complete, open the outlet door and remove the cleaned IBC container or bin.
-
Transfer the cleaned container to the intermediate holding station for storage.
Key Features and Benefits
-
Fully Automated: The PLC control system ensures consistent, unattended cleaning operations.
-
High Efficiency: The automated process minimizes downtime and increases throughput.
-
GMP Compliant: Designed with smooth surfaces, no dead corners, and no exposed screws to meet GMP standards for pharmaceutical manufacturing.
-
Versatility: Compatible with IBC containers, blending bins, and transfer bins of various specifications and types.
-
Advanced Air Handling: An integrated air handling unit ensures proper drying and contamination control.
-
Robust Construction: Durable design and stable performance ensure reliable operation.
-
User-Friendly Interface: An intuitive PLC control panel simplifies operation and programming.
-
Optimized Production Process: Automated cleaning process, streamlining production.
Why Choose Guibao
Decades of Expertise, Strong Manufacturing Strength
With four decades of pharmaceutical equipment expertise, we deliver high-standard solutions through mature processes and core technologies.
International Certifications, Assured Quality and Compliance
ISO 9001, CE, and other international certifications ensure standardized production, reliable quality, and dependable service at every stage.
University-Industry R&D, Customized Technical Support
Together with Jiangnan University, we operate an intelligent manufacturing R&D center, providing customized equipment optimization, production line upgrades, and MES/SCADA solutions for smarter operations.
Full-Lifecycle Concierge Service, Worry-Free Support Throughout
Full-lifecycle support from planning to maintenance ensures stable production. Guibao Group delivers efficient equipment and complete production lines with advanced technology and responsive service.
Get a Quick Quote
 Advanced technology provides one-stop service for your enterprise
24/7 before-sales and after-sales services
Comprehensive technical support